2026 Best Laser Cladding Machines for Global Buyers

Choosing among the 2026 Best Laser Cladding Machines for Global Buyers requires more than comparing advertised power ratings. A reliable decision begins with the application: worn shafts, turbine blades, mining teeth, oilfield components, or corrosion-resistant surfaces. Each part demands different powder chemistry, laser wavelength, spot size, deposition rate, and dilution control. A machine that repairs a 300-millimeter shaft efficiently may perform poorly on a thin aerospace edge.

Professor John N. DuPont, a widely recognized welding and cladding researcher, has emphasized a practical principle: “The key to successful cladding is control of dilution and heat input.” That principle remains relevant in 2026. Buyers should examine melt-pool stability, heat-affected-zone width, powder utilization, layer adhesion, and repeatability under production conditions. Ask for metallurgical reports, not only polished photographs.

Real experience matters.

This guide evaluates machine architecture, fiber-laser output, coaxial and lateral powder delivery, automation, monitoring systems, and post-cladding machining needs. It also considers technical support, spare-parts access, operator training, warranty terms, and regional service coverage. These details can determine whether a promising machine becomes productive equipment or an expensive installation.

Some comparisons remain imperfect. Manufacturers may measure deposition rates under different powder sizes and test conditions. Published figures can therefore mislead. Independent trials are worth the time. Buyers should test their actual alloy, geometry, and repair thickness before signing a purchase agreement. The strongest choice is rarely the machine with the highest headline power. It is the system that delivers stable, traceable, and economically defensible Laser Cladding results over many production cycles.
2026 Best Laser Cladding Machines for Global Buyers

What Is a Laser Cladding Machine and How Does It Work?

2026 Best Laser Cladding Machines for Global Buyers

What Is a Laser Cladding Machine and How Does It Work?

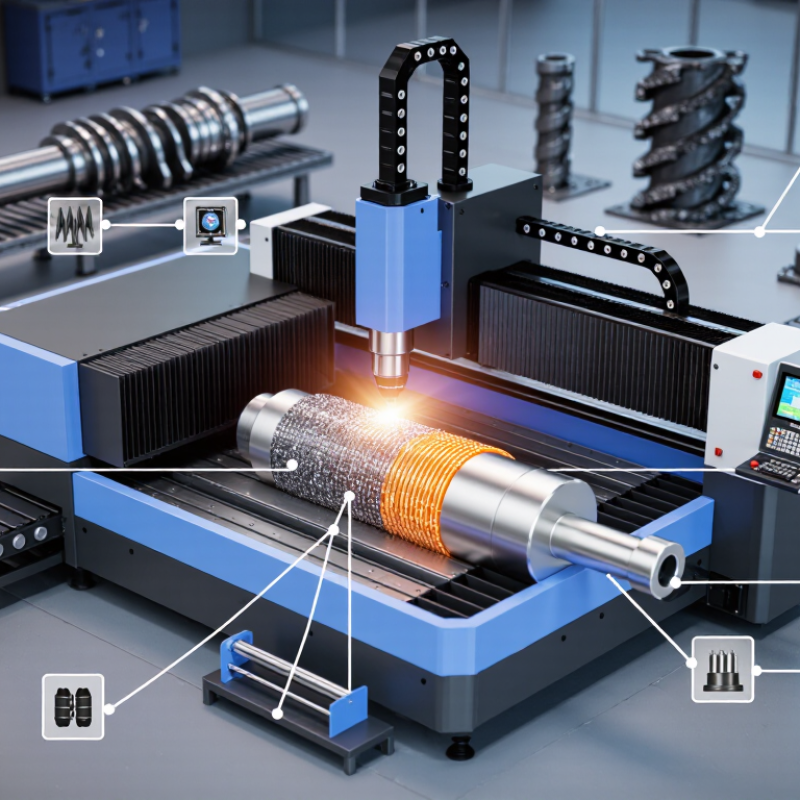
A laser cladding machine repairs or protects metal surfaces with a precisely controlled laser beam. It places new material over a base component. The process creates a metallurgical bond, not merely a surface coating. Typical feedstock includes metal powder or wire. The selected material depends on wear, corrosion, temperature, and impact requirements.

During operation, the laser forms a small molten pool on the substrate. A nozzle delivers powder or wire into this pool. Shielding gas limits oxidation around the heated area. As the laser moves, the material cools and forms a dense deposited track. Successive tracks overlap to build the required thickness. Control matters.

Experienced technicians adjust laser power, travel speed, feed rate, and gas flow together. Excessive heat can increase dilution or distort a precision part. Insufficient energy may cause weak bonding or trapped pores. Robotic or CNC movement improves repeatability across complex surfaces. However, automation cannot replace correct parameter development.

For global buyers, working envelope, material compatibility, powder recovery, and service documentation deserve careful review. A first pass may look excellent, yet hidden porosity can remain. Inspection methods such as dimensional checks, hardness testing, and metallographic analysis reveal more. The process is powerful, but less forgiving than promotional descriptions suggest. Costs also depend on operator skill, consumables, maintenance, and local technical support.
2026 Best Laser Cladding Machines for Global Buyers

What Is a Laser Cladding Machine and How Does It Work?

A laser cladding machine uses a focused laser to create a controlled melt pool on a metal surface while powder or wire is added as the coating material. The deposited material solidifies into a metallurgically bonded layer with relatively low dilution. The representative thickness ranges below show common industrial use cases; actual results depend on laser power, material, powder or wire feed rate, travel speed, and the required surface finish.

Key Technologies Used in Modern Laser Cladding Systems

2026 Best Laser Cladding Machines for Global Buyers

Modern laser cladding systems rely on several technologies working together. Fiber lasers deliver concentrated heat with stable power and low thermal distortion. Coaxial powder nozzles feed metal particles into the melt pool from multiple directions. This supports consistent coating quality during complex tool paths. Wire feeding can reduce powder waste for large components.

Real-time monitoring is becoming essential for global buyers. Cameras, pyrometers, and melt-pool sensors track temperature, geometry, and surface changes. Closed-loop controls can adjust laser power or feed rate during production. The result is better repeatability across batches and operators. Still, sensor data needs careful calibration. Dirty lenses can create false confidence.

Motion systems also matter. Robotic arms provide flexible access, while CNC platforms offer predictable positioning. Advanced beam shaping helps control penetration and coating width. Water or air cooling protects optics and nearby components. Buyers should also examine software records, maintenance access, spare-part availability, and operator training. A machine may look impressive during a demonstration, yet perform poorly with reflective alloys or uneven substrates. Trial cladding with the actual material is wiser than relying on brochures. Small process errors become visible as pores, cracks, or weak bonding. That lesson is easy to miss.

How to Compare Laser Cladding Machines for Global Applications

2026 Best Laser Cladding Machines for Global Buyers

How to Compare Laser Cladding Machines for Global Applications

Global buyers should compare performance, not laser wattage alone. A larger laser does not guarantee better repair quality. Review deposition rate, powder utilization, spot size, and thermal control. The Wohlers Report 2024 valued the global additive manufacturing industry at approximately 20.035 billion US dollars in 2023. This growth increases demand for reliable metal repair and surface enhancement systems. However, laser cladding remains highly application-dependent.

Ask suppliers for test coupons using your actual alloy and substrate. Check hardness, dilution, porosity, bond strength, and heat-affected zones. Request measured results, not attractive averages. A machine for turbine repair may differ greatly from one for mining rollers. Closed-loop monitoring can improve repeatability, but sensor claims need practical evidence. Compare software traceability, operator training, spare-part access, and regional service response. These details affect uptime more than brochure specifications. Sometimes, I still find the cheapest lifetime estimate too optimistic.

Tips: Build a weighted comparison sheet. Give process quality, service coverage, and total operating cost equal importance. Confirm electrical compatibility for each destination. Examine powder safety documentation and material traceability. Ask whether the system supports wire or powder, because changing feedstock later may be expensive. The ASTM Additive Manufacturing Center of Excellence emphasizes process qualification and data consistency. Follow that discipline before approving production equipment. No spreadsheet replaces a test coupon.

Top Machine Types for Different Materials and Repair Tasks

2026 Best Laser Cladding Machines for Global Buyers

Top Machine Types for Different Materials and Repair Tasks

Choosing a laser cladding machine starts with the material, not the brochure. For steel shafts, gears, and hydraulic rods, a coaxial powder system offers controlled deposition and flexible alloy changes. Wire-fed systems suit larger repairs because wire costs less and creates fewer airborne particles. They may need more heat control, though. For nickel alloys and cobalt-based overlays, a high-power fiber laser improves bonding and deposition speed. Stainless steel often benefits from precise, low-heat processing, especially around thin edges.

Industry demand is expanding. The 2025 Wohlers Report recorded global additive manufacturing revenue of about $24.2 billion in 2024, a 9.1% annual increase. This figure covers more than cladding, but it reflects wider confidence in digital repair and metal deposition. Buyers should also examine laser power, spot size, powder efficiency, axis travel, and closed-loop temperature control. A machine that looks fast may waste material during unstable starts. I have seen this overlooked.

Tips: Match the machine to the repair zone. Use wire for long, heavy rebuilds. Choose powder for small, complex surfaces. Request test coupons using your actual alloy and geometry. Measure dilution, hardness, porosity, and machining allowance. Do not trust one successful sample. Repeat it. Calibration quality, operator skill, and software settings can change results more than expected.

2026 Best Laser Cladding Machines for Global Buyers - Top Machine Types for Different Materials and Repair Tasks

Machine Type Typical Laser Power Material Feedstock Suitable Materials Typical Deposition Rate Best Repair or Production Tasks Recommended Workpiece Size Main Buying Advantages
Standard Powder-Fed CNC Cladding Cell 2–6 kW fiber laser Metal powder, commonly 45–150 μm Carbon steel, stainless steel, tool steel, nickel alloys, cobalt alloys 0.3–2.0 kg/h, depending on alloy and layer size Shaft restoration, sealing surfaces, bearing seats, dimensional correction, wear-resistant overlays Small to medium components; commonly up to approximately 1,000 mm turning diameter or comparable travel Good balance of precision, automation, repeatability, and material flexibility
High-Power Powder-Fed Cladding System 6–12 kW fiber or diode laser Metal powder, typically 50–180 μm Nickel-based superalloys, stainless steels, cobalt alloys, iron-based wear alloys 1.5–6.0 kg/h in large-track applications Large mining parts, energy components, hydraulic cylinders, thick wear layers, high-volume remanufacturing Medium to large parts with extended machine travel or rotary positioning Higher productivity and thicker deposition; suitable for industrial repair throughput
High-Speed Laser Cladding Machine 1–4 kW fiber laser Fine metal powder, commonly 20–80 μm Stainless steel, nickel alloys, iron-based alloys, selected carbide-containing powders 0.5–3.0 kg/h; high traverse speeds are used for thin layers New-part surface enhancement, sealing diameters, corrosion barriers, thin wear-resistant coatings Small to medium cylindrical or planar components Lower heat input and faster coverage for controlled surface treatment with limited distortion
Wire-Fed Laser Metal Deposition System 2–12 kW fiber or diode laser Metal wire, commonly 0.8–1.6 mm diameter Carbon steel, stainless steel, nickel alloys, titanium alloys, aluminum alloys with suitable process control 0.5–8.0 kg/h, depending on wire size, power, and geometry Large-part build-up, edge restoration, aerospace tooling, near-net-shape deposition, material-efficient repair Medium to very large parts using gantry, robot, or multi-axis positioning High material utilization and lower consumable cost than powder-fed processing
Five-Axis Robotic Cladding Cell 2–8 kW fiber laser Powder or wire, selected according to the deposition head Steels, nickel alloys, cobalt alloys, titanium alloys, aluminum alloys with qualified parameters 0.3–5.0 kg/h, depending on feedstock and toolpath Complex blades, molds, dies, impellers, curved surfaces, localized repair of irregular geometries Irregular parts requiring multi-axis access and flexible orientation Excellent accessibility and path flexibility for complex geometries
Large Gantry Laser Cladding Machine 4–12 kW fiber or diode laser Powder or wire Carbon steel, low-alloy steel, stainless steel, nickel alloys, wear-resistant iron-based alloys 1.0–8.0 kg/h, subject to process configuration Rolls, shafts, pressure-vessel components, construction equipment, large hydraulic and energy parts Large components several meters in length or diameter, subject to machine design Rigid structure, long travel, and efficient coverage of large repair areas
Compact Manual or Portable Cladding Unit 0.5–2 kW fiber laser Fine powder or specialized wire, depending on the applicator Stainless steel, nickel alloys, cobalt alloys, and selected tool steels 0.05–0.5 kg/h On-site restoration of small shafts, molds, sealing edges, precision tooling, and localized defects Small components or accessible local repair zones Lower installation requirements and practical for maintenance departments with varied job sizes
Technical note: The figures are typical engineering ranges rather than guaranteed machine specifications. Actual deposition rate, layer thickness, dilution, heat input, and dimensional accuracy depend on laser wavelength, spot size, powder or wire chemistry, feed rate, substrate condition, shielding gas, travel speed, toolpath, and part geometry. A process qualification test should be completed before production purchasing.

Buying, Installation, and Support Factors for International Buyers

For international buyers, a laser cladding machine should match the repair task, material, and production scale.

Start with the alloy, substrate, and required layer thickness. Match laser power, powder feeder range, nozzle design, and work envelope carefully. Request test results using your own materials. Generic samples can hide poor bonding or excessive dilution. Ask for measured deposition rate, hardness, and surface finish. Details decide uptime.

Installation planning deserves equal attention. Confirm electrical standards, compressed-air quality, cooling requirements, floor loading, and ventilation before shipment. Request factory drawings with service clearances and lifting points. Installation is not plug-and-play.

A remote commissioning session can verify beam alignment, powder flow, shielding gas, and safety interlocks. Local technicians may reduce delays, but their availability should appear in the contract. Include operator training, recorded procedures, troubleshooting examples, and cleaning schedules. Translated manuals may miss practical details. Have an engineer review them before production.

Support terms matter after the crate arrives. Check warranty coverage, response times, software access, spare-part lead times, and escalation channels across time zones. Clarify customs documents, import responsibilities, and local service limits. Ask whether diagnostic logs can be shared securely without exposing production data. Keep critical nozzles, lenses, filters, and feeder seals on site. A realistic acceptance test should define uptime, coating quality, and repeatability.

Do not judge suppliers by price alone. The cheapest installation can become the most expensive delay.

keep me informed

Subscribe

By clicking SEND means that you agree to our Terms & Conditions, Privacy and Cookie Policies.